Material guide · Exterior panels
PDCPD vs SMC, FRP and thermoformed ABS for low-volume panels
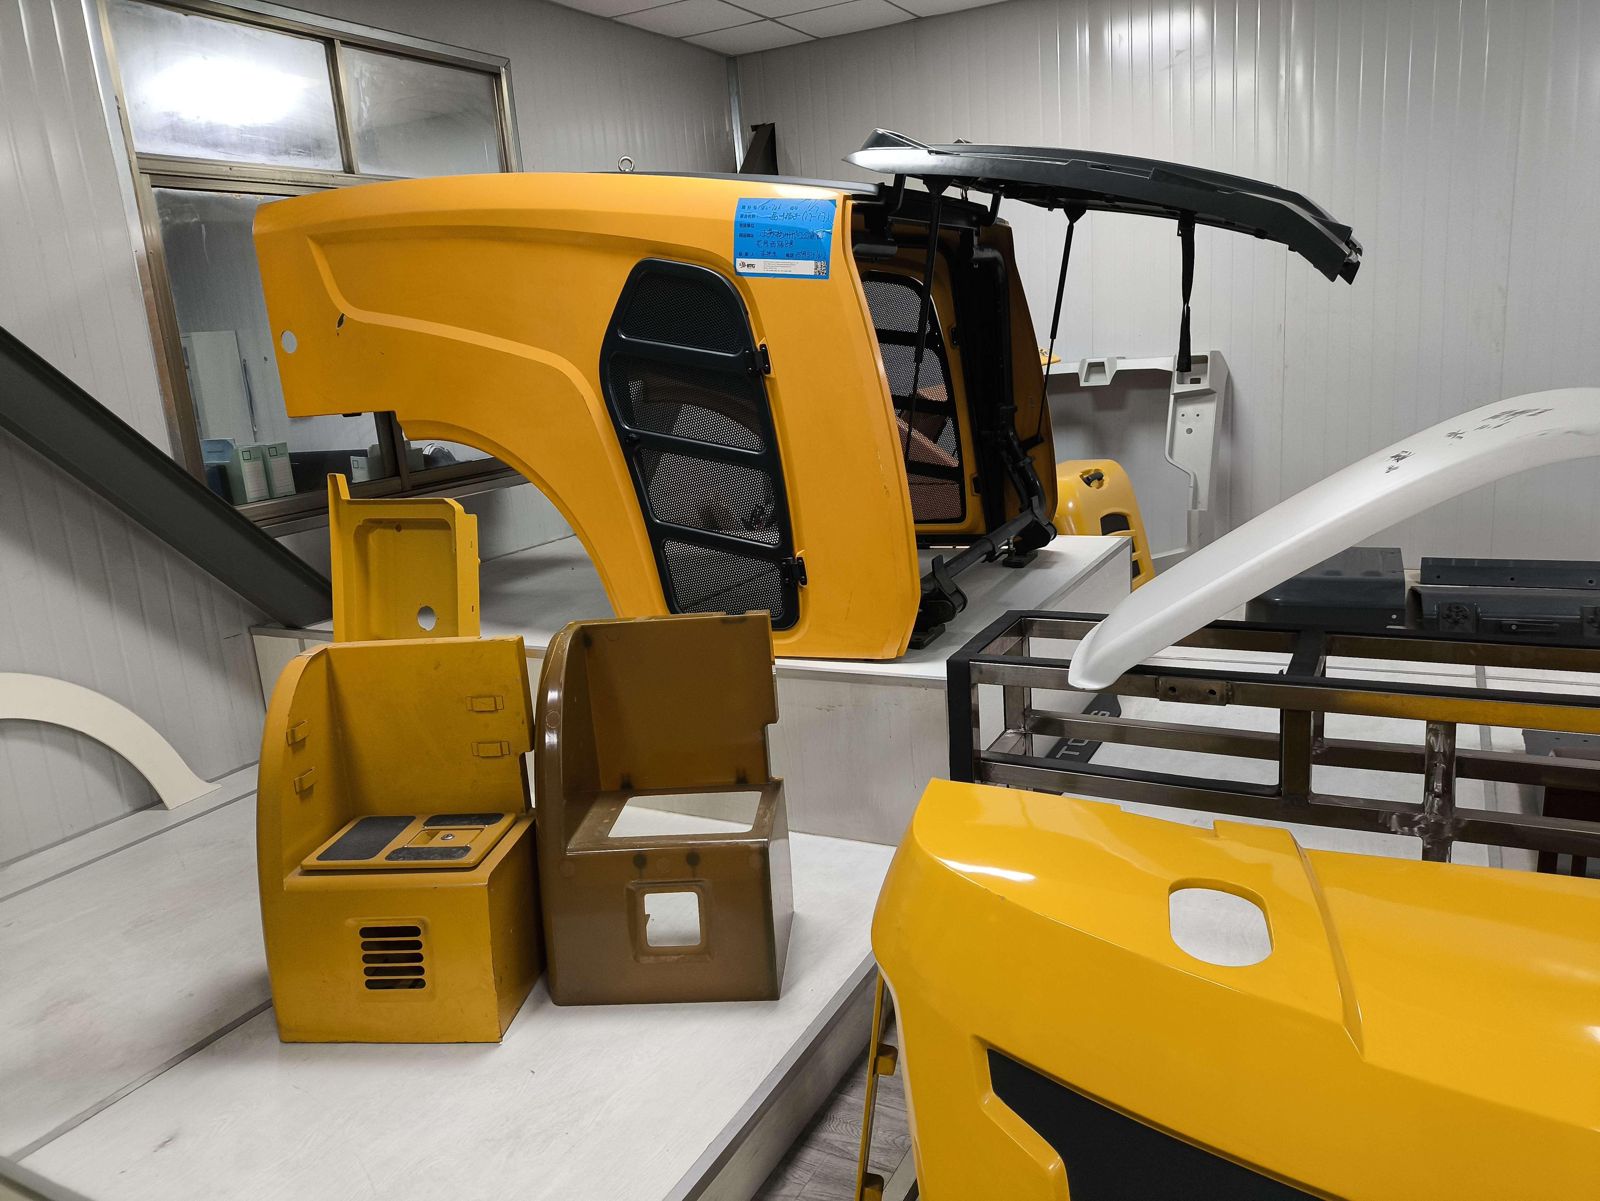
Hoods, fenders and covers for tractors, excavators and trucks are built in hundreds to a few thousand sets a year. At those volumes the choice of material and process decides most of the part cost. This is how the common options compare.
The numbers side by side
| Property | PDCPD (RIM) | ABS (vacuum forming) | PP (injection) | SMC | Sheet steel |
|---|---|---|---|---|---|
| Density, g/cm³ | 1.03 | 1.04 | 0.98 | 1.8 | 7.87 |
| Flexural modulus, MPa | 1,700 | 1,600 | 1,200 | 11,000 | 210,000 |
| Thermal expansion, 10⁻⁵ /°C | 7.5 | 10 | 10 | 2 | 0.01 |
| Heat deflection temp., °C | 115 | 78 | 69 | >200 | – |
| Impact behaviour | Best; flexes and recovers | Good | Fair | Cracks | Dents |
| Wall thickness changes | Easy | Not possible | Possible | Possible | Limited |
| Ribs and bosses | Easy | Not possible | Possible | Possible | Not possible |
| Molded-in inserts | Yes | No | Yes | No | No |
| Tooling cost | Low to medium | Lowest | High | High | Highest |
| Best annual volume | Low to medium | Low to medium | High | High | High |
| Chemical resistance | Excellent (acid, alkali) | Good | Good | Good | Poor (rust) |
Typical values for general-purpose grades. Flame-retardant PDCPD grades reach UL94 V-0; standard grades do not.
Where PDCPD wins
- Large parts in the hundreds per month. RIM runs at 1 to 3 bar in the cavity, so the mold can be cast or machined aluminium. Below roughly 500 parts a month, total part cost is usually lower than SMC or injection-molded PP, where the steel tool dominates.
- Parts that get hit. Fenders, bumpers and lower covers on field machines take impacts. PDCPD flexes and returns to shape where SMC cracks and steel dents.
- Complex one-piece designs. Ribs, bosses, thick-to-thin transitions and molded-in nuts come out of one shot. A steel hood that needs welded brackets often becomes a single PDCPD part.
- Weight. At 1.03 g/cm³, PDCPD is close to half the weight of SMC for the same wall thickness, and a fraction of steel.
Where another material is the better choice
- High stiffness or high heat. SMC is more than six times stiffer and survives over 200 °C. Panels close to the exhaust or carrying structural loads without ribs are often better in SMC.
- Very high volumes. Above a few thousand parts a month, injection-molded PP or SMC lowers the part price, because the higher tooling cost is spread over more parts.
- Tight dimensions over a wide temperature range. PDCPD expands about four times more than SMC. Long panels need slotted mounting holes and gap allowance.
- Prototype or a few dozen parts. Vacuum-formed ABS has the cheapest tooling, if the part has no ribs and uniform walls.
Questions to settle before choosing
- How many parts per year, and for how many years?
- What is the maximum service temperature near the part?
- Will the part be hit, stepped on or pressure-washed?
- Do you need ribs, bosses or inserts that would otherwise be welded or bonded on?
- Will the part be painted, and in what process?
Not sure PDCPD fits your part? Send the 3D data and annual volume. We will tell you honestly whether PDCPD-RIM or another process is the better choice. Contact us.